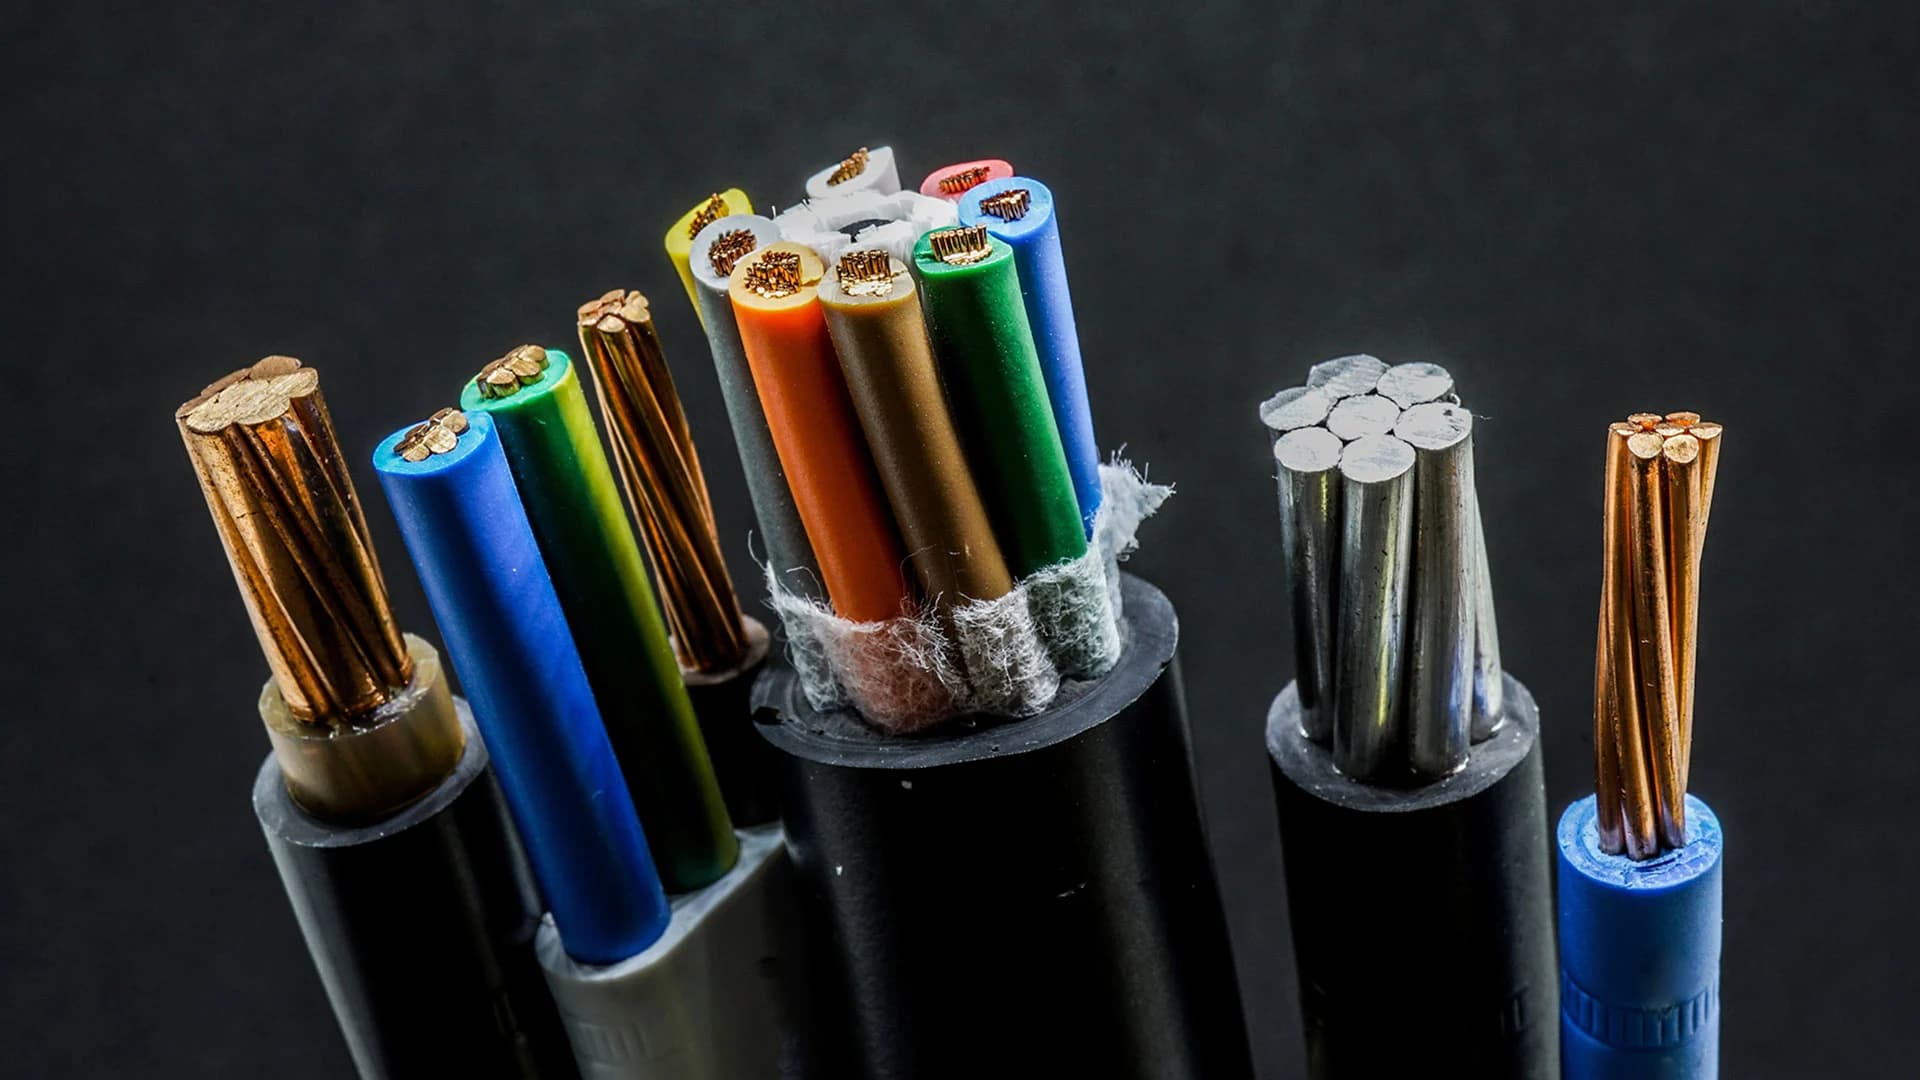
Reliable Electrical Solutions for the Food & Beverage Industry
Connecting, Protecting, and Organising Systems in Food & Beverage Facilities
At Bharat Trading Company (BTC), we understand the special demands of food and beverage manufacturing environments, where safety, hygiene, and uninterrupted operations are the key. That’s why we supply high-quality electrical cables, control wiring, accessories, and cable management systems that are specially built to perform reliably in challenging production and packaging conditions. Our solutions are designed to support your smooth, continuous operations while meeting industry standards related to cleanliness, durability, and performance. Our overall aim is to help manufacturers focus on efficiency, quality, and compliance with confidence.
What Is the Food & Beverage Industry and How Does BTC Support It?
Supplying Best-in-Class Electrical Infrastructure Built for Hygiene, Heat, and Non-Stop Operations
The food and beverage industry is all about bringing safe, high‑quality products to people every day. It covers everything from processing raw ingredients to manufacturing, packaging, and distributing food and drinks. This is all done under strict hygiene and safety standards. Because even the smallest disruption can affect production, this industry relies on systems that are reliable, efficient, and built to last. That’s where Bharat Trading Company (BTC) comes in.
We proudly support this industry by supplying best-in-class electrical solutions that help keep these plants running safely and smoothly. Our range includes durable power cables, precise control and instrumentation wiring, and accessories designed to handle heat, moisture, and demanding environments. From lugs and glands to heat‑shrink insulation and organised cable management solutions, we ensure that your operations stay safe, compliant, and continuously powered. With BTC, you don’t just get products, you get peace of mind knowing your plant is supported by electrical solutions built for performance and reliability.
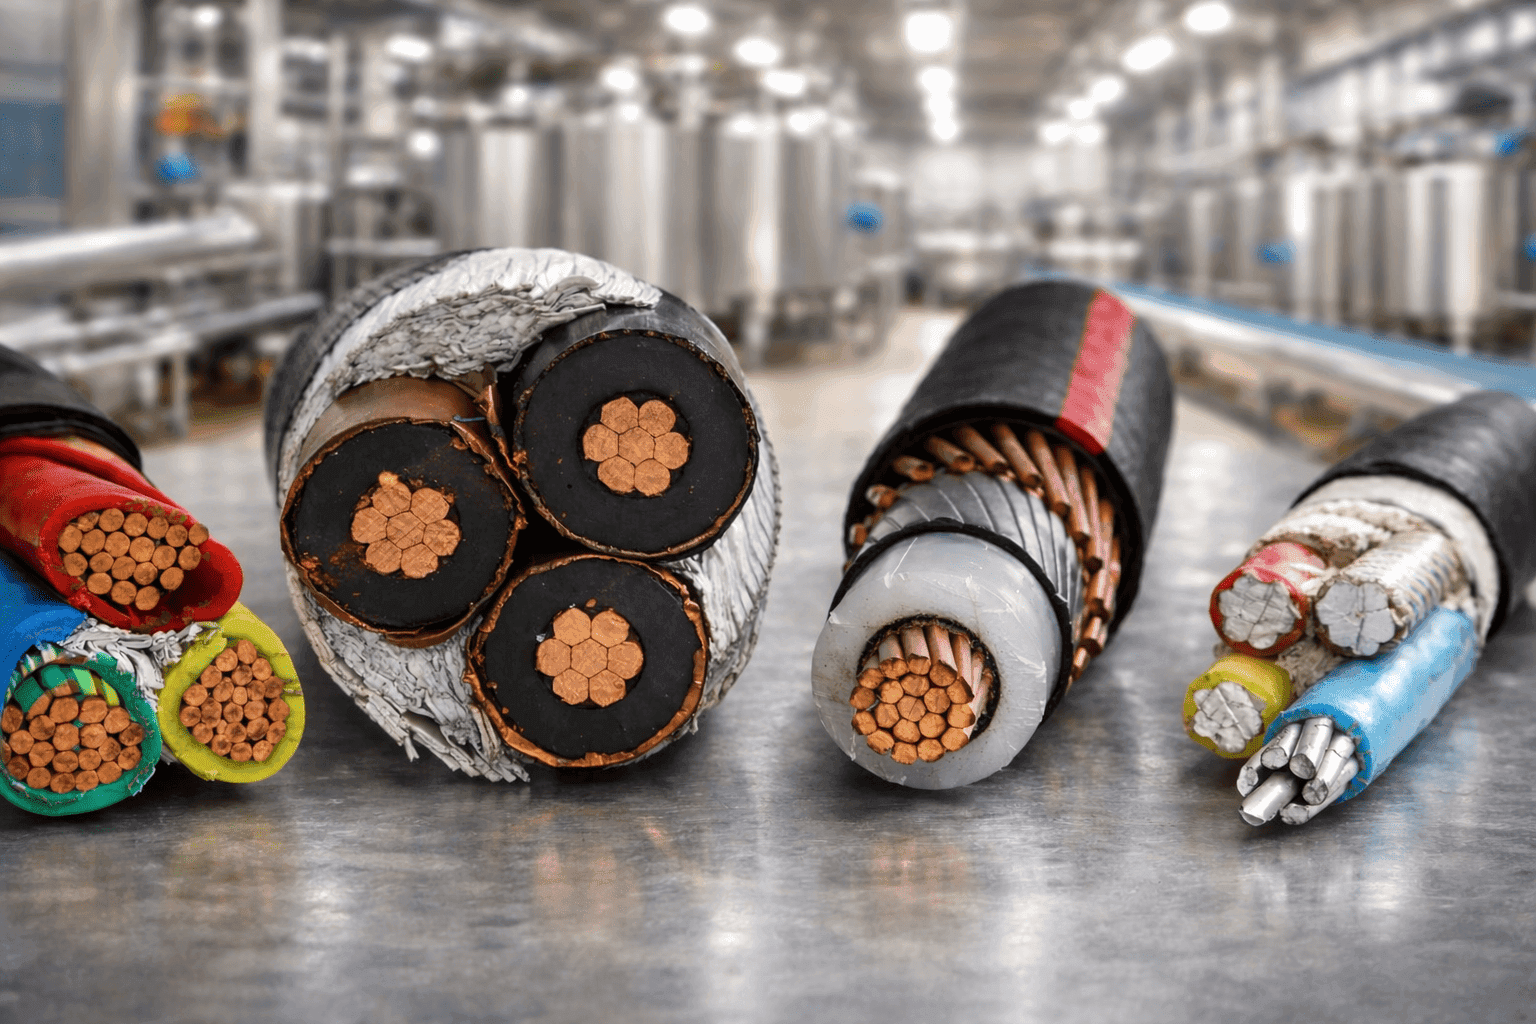
Where BTC Products Are Used in Food & Beverage Facilities
Electrical systems play a vital role in every corner of a food and beverage plant. From preparation to packaging, BTC’s products are trusted to keep operations safe, reliable, and efficient. Here’s how they support different areas:
Food Processing and Preparation Areas
In every kitchen mixer, grinders, ovens, fryers, and other heavy‑duty equipment need stable power to run smoothly. BTC’s cables and wiring solutions ensure these machines operate safely and consistently, even in demanding environments.
Product Categories for Construction Projects
Engineered for high-rise risers, concealed conduits, underground mains, and electrical panel rooms. All lines supplied strictly from Tier-1 OEM factory allocations with full test certification.

Control & Instrumentation Cables
Modern food and beverage plants rely on automation and precise control. BTC’s control and instrumentation cables ensure accurate and reliable signal transmission for sensors and control systems.
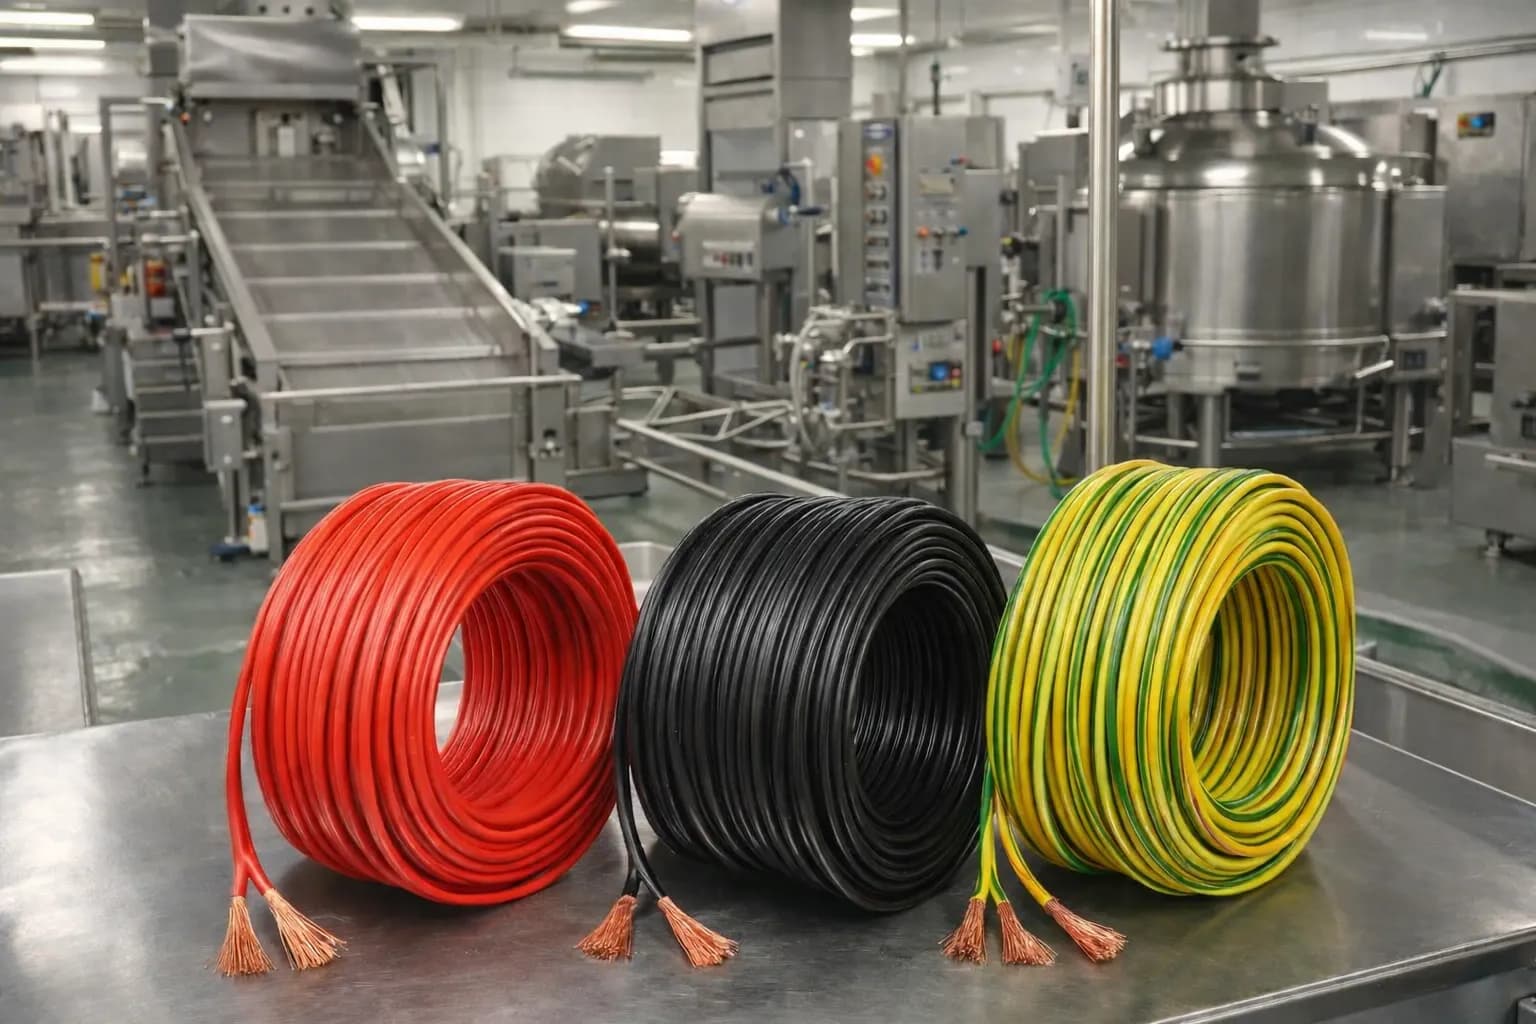
Flexible Industrial Wires & Cables
Designed for machines and production areas that require constant movement, our flexible industrial cables adapt without damage or performance loss.
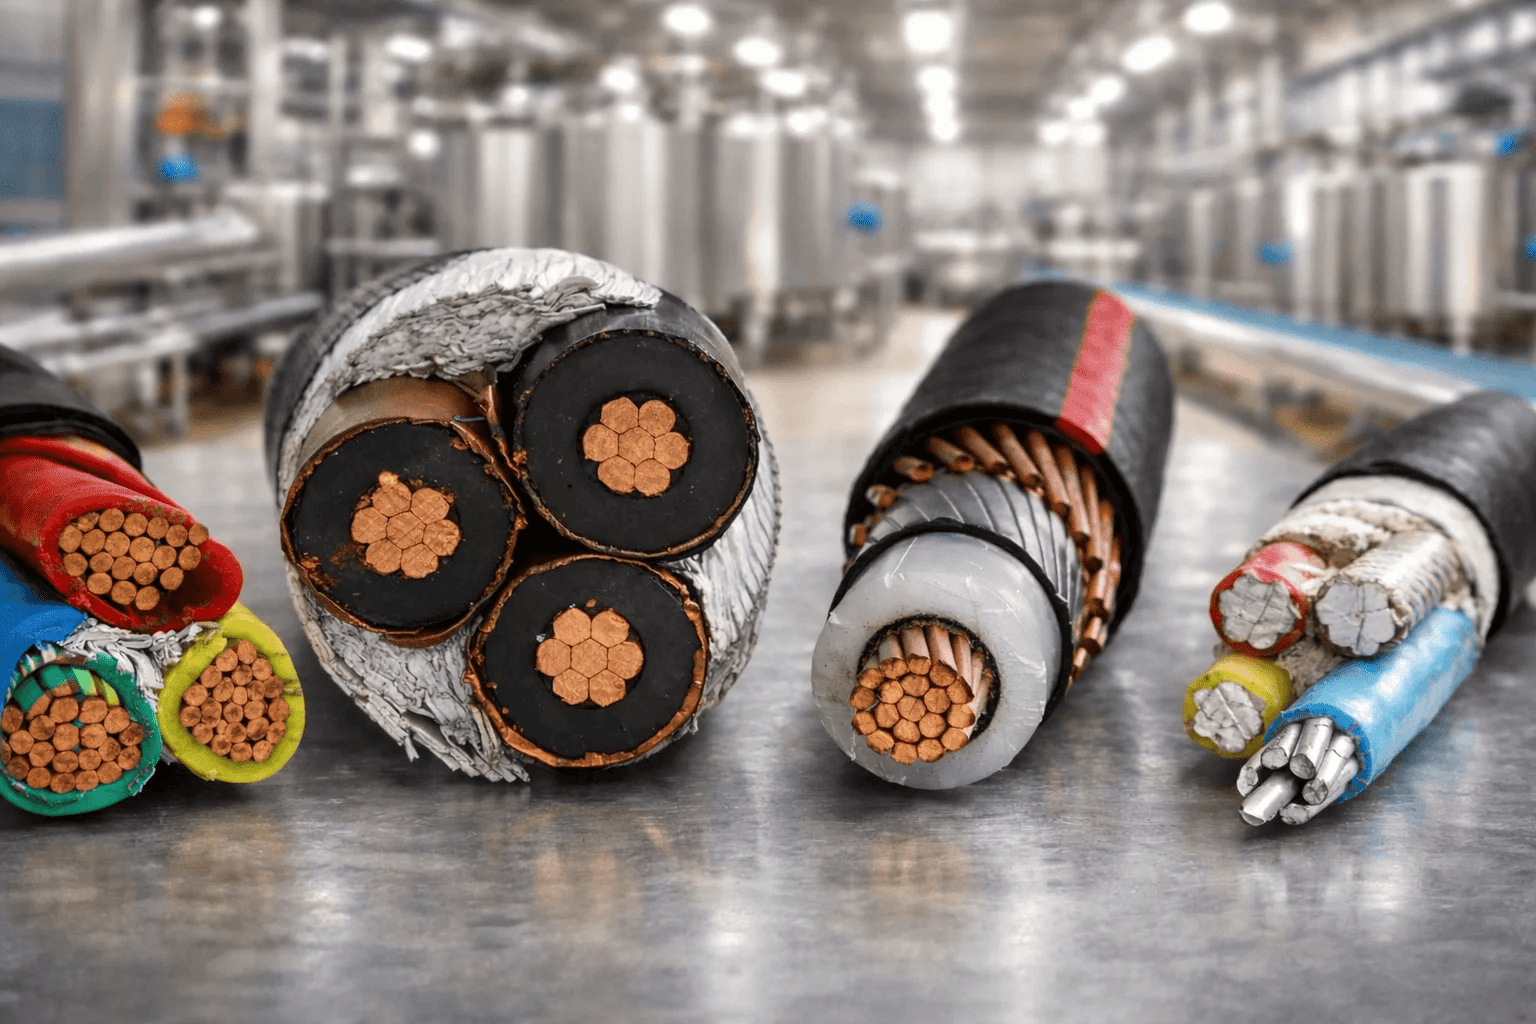
Armoured & Unarmoured Power Cables
BTC power cables deliver dependable electricity for indoor and outdoor installations, offering the right protection based on the application.
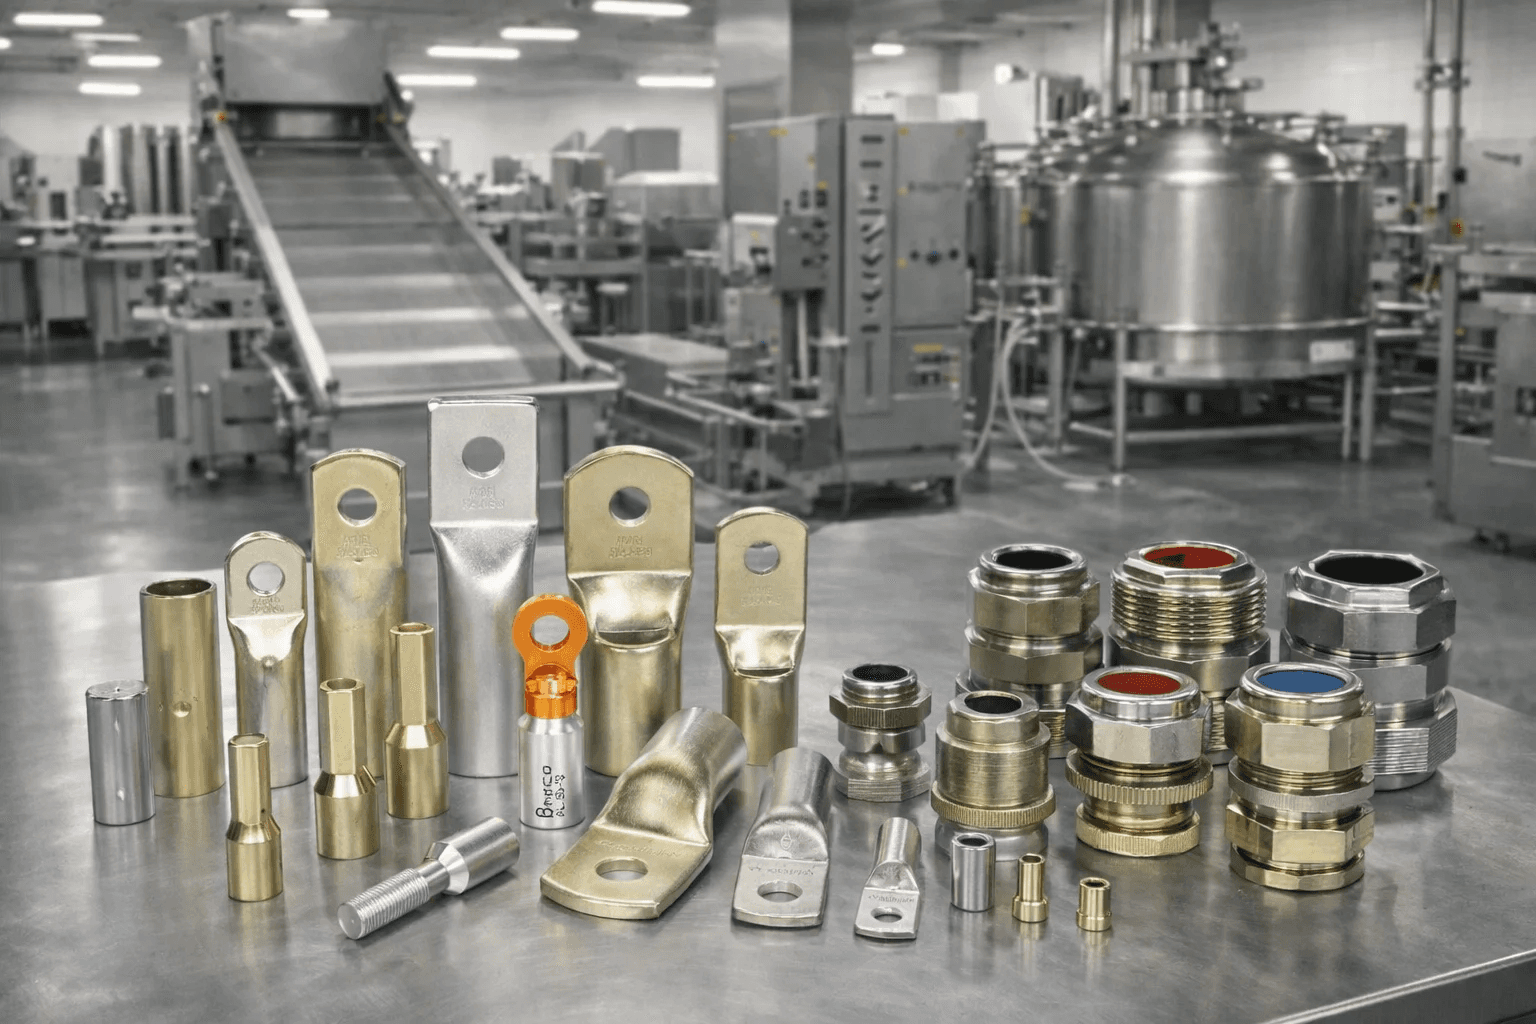
Cable Lugs & Glands (Moisture-Resistant)
Designed for washdown and wet environments, BTC’s cable lugs and glands protect connections from water, dust, and vibration.

Heat Shrink Sleeves & Insulation Accessories
Heat shrink sleeves enhance electrical safety by insulating, protecting, and clearly identifying cables in food-grade environments.
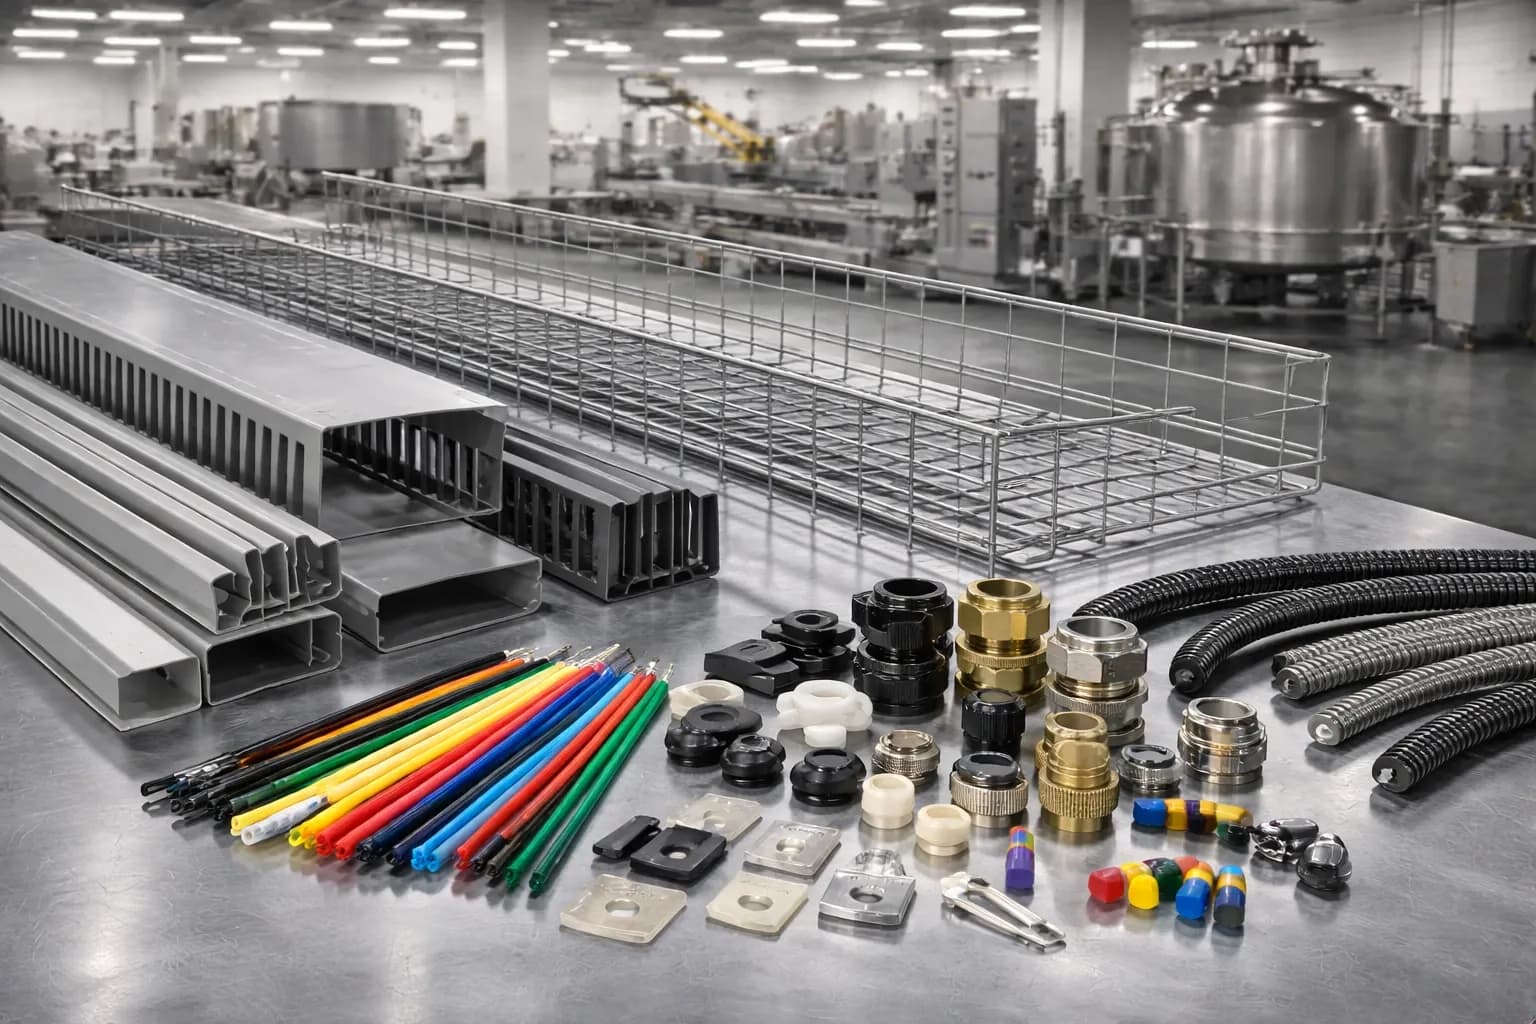
Cable Management Systems
Organised cabling improves hygiene, safety, and maintenance efficiency. BTC’s ducts, trays, and conduits keep wiring secure and accessible.
Control & Instrumentation Cables
Modern food and beverage plants rely on automation and precise control. BTC’s control and instrumentation cables ensure accurate and reliable signal transmission for sensors and control systems.
Flexible Industrial Wires & Cables
Designed for machines and production areas that require constant movement, our flexible industrial cables adapt without damage or performance loss.
Armoured & Unarmoured Power Cables
BTC power cables deliver dependable electricity for indoor and outdoor installations, offering the right protection based on the application.
Cable Lugs & Glands (Moisture-Resistant)
Designed for washdown and wet environments, BTC’s cable lugs and glands protect connections from water, dust, and vibration.
Heat Shrink Sleeves & Insulation Accessories
Heat shrink sleeves enhance electrical safety by insulating, protecting, and clearly identifying cables in food-grade environments.
Cable Management Systems
Organised cabling improves hygiene, safety, and maintenance efficiency. BTC’s ducts, trays, and conduits keep wiring secure and accessible.
Control & Instrumentation Cables
Types and Categories of Food & Beverage Electrical Systems
Food and beverage facilities rely on a wide range of electrical systems to keep operations running smoothly, safely, and efficiently. At Bharat Trading Company (BTC), we understand that each area of a plant has unique electrical needs. That’s why we offer the right cables, components, and accessories suited for every application.
Core Production Electrical Systems
Processing Lines
The heart of any food facility is its processing line. These systems require reliable, durable cables that can handle constant operation, heat, and frequent cleaning. BTC’s electrical components deliver steady power to your mixers, grinders, ovens, and other equipment helping to maintain quality and speed in production.
Packaging System Electrical Networks
Once products are ready, packaging systems take over. Our wiring and accessories ensure that packaging machines operate reliably, keeping output fast, accurate, and hygienic.
Cold Storage Electrical Systems
Temperature control is critical in food and beverage operations. Cold storage areas require special demands on electrical systems due to low temperatures and moisture. BTC supplies durable cables and protective accessories designed for cold storage environments, ensuring uninterrupted power to refrigeration units and helping maintain product freshness and quality.
Utilities, Automation & Safety Networks
Utility and Boiler Electrical Systems
Behind the scenes, utility and boiler systems keep plants running 24×7. Utilities such as boilers, compressors, and water treatment units operate in high-temperature and demanding conditions. BTC’s heat-resistant and heavy-duty electrical components are built to withstand these environments while supporting safe and efficient energy use.
Automation and Control Networks
Today, modern food and beverage plants rely heavily on automation for improved efficiency and quality control. BTC supports these systems with control and instrumentation cables that enable smooth communication between PLCs, sensors, and machines, helping plants achieve better accuracy and process control.
Safety and Monitoring Systems
Reliable electrical systems are essential for safety in food and beverage facilities. BTC’s cabling and accessories support alarms, emergency shut-offs, and monitoring systems to ensure compliance and protect both workers and equipment.
Why Electrical Reliability Matters in the Food & Beverage Industry?
In the food and beverage industry, reliability isn’t just about keeping the lights on and cooking, it's about protecting products, people, and processes. Even a short electrical disruption can cause production delays, spoil batches, create safety risks, or lead to non‑compliance with strict regulations. Every part of a plant from mixers and ovens to chillers, conveyors, and packaging machines depends on stable power and precise control to run smoothly. When electrical systems fail, the impact is immediate and costly. That’s why high‑quality electrical components make all the difference. They help prevent unplanned shutdowns, safeguard sensitive equipment, and support hygienic operations by ensuring all installations are safe, organised, and built to last.
BTC: Your Trusted Electrical Partner in the Food & Beverage Industry
In the food and beverage industry, every detail matters. From maintaining strict hygiene and safety standards to ensuring uninterrupted production, reliable electrical systems play a crucial role in keeping operations efficient, compliant, and running without downtime. At Bharat Trading Company (BTC), we understand these unique challenges. That’s why we supply high‑quality cables, accessories, and wiring solutions designed specifically for food processing plants and beverage manufacturing facilities. With our reliable products and years of industry expertise, BTC has become a trusted partner for companies across Pune, Maharashtra, and all of India.
Explore Solutions
- Moisture-resistant cables for washdown areas
- Flexible wiring for high-speed machines
- Fire-retardant cables for safety compliance
- Sealed cable glands & heavy-duty lugs
How We Support Your Facility
- Application-matched product recommendations
- Batch test certificates & compliance reports
- Ready inventory for rapid scheduled dispatch
- Dedicated engineering technical support
Comparison: Electrical Options in Food & Beverage Applications
Choosing the right type of cable is especially important in food and beverage facilities, where safety, hygiene, and reliability are non‑negotiable. Here’s a quick comparison to help you see which options work best in different situations.
| Application Area | Better Option | Why It Matters |
|---|---|---|
| Washdown & Moisture-Prone Zones | Moisture-Resistant Cables | Food and beverage plants go through frequent washdowns to maintain hygiene. Standard cables can fail when exposed to water. Moisture-resistant cables ensure durability and safety during frequent cleaning. Unlike standard cables, they don’t degrade quickly, making them a safer and longer-lasting choice for wet and washdown areas. |
| Moving Machinery & Equipment | Flexible Cables | Many machines in processing units move, vibrate, or operate continuously. Flexible cables bend easily without cracking or breaking. Unlike rigid wiring, they move with machinery, reducing wear, preventing breakdowns, and minimizing maintenance issues. |
| Enclosed Processing Areas | Fire-Retardant Cables | Fire-retardant cables slow the spread of fire and produce less smoke during overheating. Conventional PVC insulation may not offer sufficient protection. These cables add an extra layer of safety, protecting both workers and critical equipment in confined spaces. |
By matching the right cable to the right environment, food and beverage companies can reduce risks, improve efficiency, and keep operations running smoothly.
Key Challenges Faced in Food & Beverage Electrical Systems
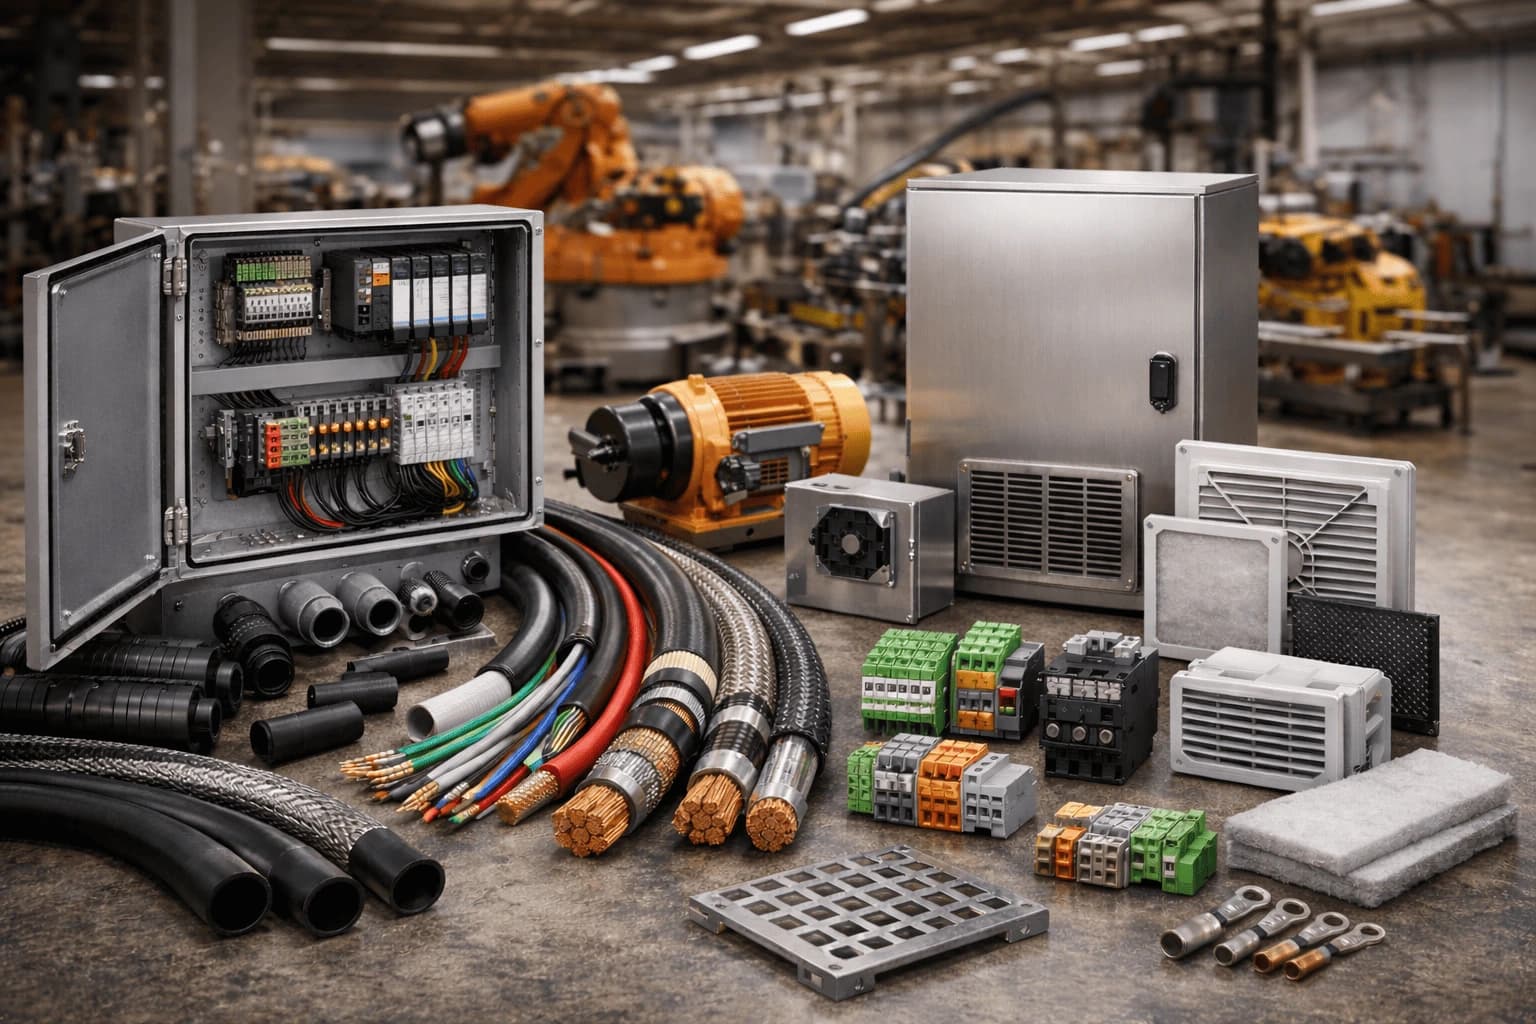
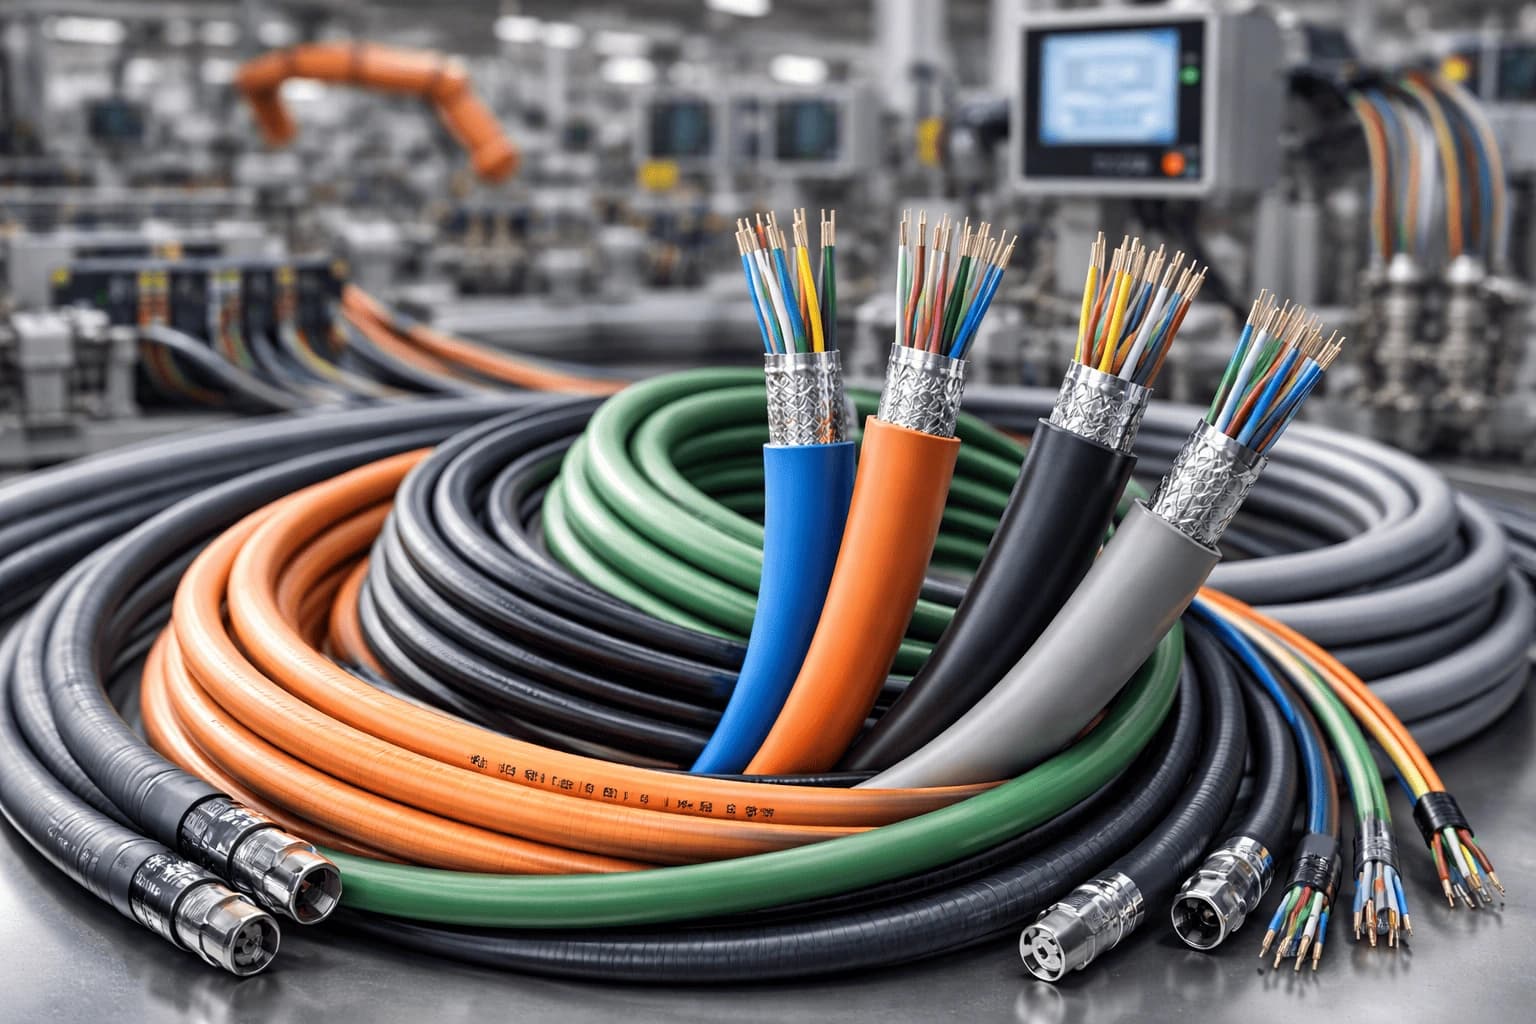
Food and beverage facilities operate under rigorous production schedules and harsh hygiene regimens. Addressing these challenges requires engineered electrical components designed for maximum durability.

Key Challenges Faced in Food & Beverage Electrical Systems
Food and beverage facilities operate under rigorous production schedules and harsh hygiene regimens. Addressing these challenges requires engineered electrical components designed for maximum durability.
Food processing areas are always exposed to water, steam, and cleaning chemicals due to routine washdowns and sanitation processes. If electrical components are not properly protected, this exposure can lead to corrosion, short circuits, and premature failures, resulting in costly downtime.
Who Needs These Food & Beverage Electrical Solutions?
Reliable electrical systems are essential across the food and beverage industry, and every operational stakeholder depends on them in unique ways directly or indirectly.

Supplying high-reliability, washdown-rated electrical products Pan-India.
Maintaining consistent output while adhering to rigorous daily sanitation and hygiene inspections.
Safe, dependable electrical infrastructure that withstands washdowns and provides stable power to mixers, cookers, and fryers without interruptions.
Key Features and Benefits of BTC Food & Beverage Solutions
At Bharat Trading Company (BTC), we understand that food and beverage facilities operate in tough conditions and require high-quality electrical components. That’s why our solutions are designed to support safety, hygiene, and efficiency while delivering reliable, long-lasting performance.
Built to handle moisture and washdowns
Food and beverage plants require frequent cleaning and they are frequently in contact with water and chemicals. BTC’s moisture-resistant insulation helps to safeguard electrical wiring solutions during regular washdowns. This reduces the overall risk of damage and ensures smooth, uninterrupted operations.
Reliable performance in high-heat areas
High temperatures are common in kitchens, bakeries, and beverage plants. BTC’s heat-resistant cables are designed to perform reliably even in hot environments, helping to prevent breakdowns and extending the overall life of electrical installations.
Enhanced safety with fire-retardant materials
Safety is a top priority in any processing facility. At BTC we only use fire-retardant materials in our electrical components. This helps to reduce fire risks, adding an extra layer of protection for people, equipment, and the facility as a whole for a safer workplace.
Flexible wiring for modern machinery
Many food and beverage machines operate in tight spaces and require regular movement. BTC’s flexible wiring solutions make installation easier and support machine movement without putting stress on the cables, improving durability and performance over time.
Clean and organised cable management
Cleanliness is key in food production, and well-organised cabling plays a big role in maintaining cleanliness and efficiency. BTC’s cable management solutions help keep wiring neat and accessible, simplifying maintenance and ensuring the facility stays hygienic.
Step-by-Step: How Electrical Systems Work in Food & Beverage Plants
From raw intake to packaging, discover how power and control flow seamlessly through every critical stage of a modern processing plant.
Power supply and distribution
Every plant starts with a steady supply of electricity. Power is brought into the facility and then distributed across different processing zones through our strong and well-insulated cables. This ensures that each section of the plant receives the right amount of power without interruptions or overloads.
Real Use Cases and Industry Examples
At Bharat Trading Company (BTC), we don’t just supply electrical components — we deliver solutions that solve real challenges for food and beverage businesses across India.
Food Processing Plant
Challenge: Facing frequent cable damage and performance issues due to daily high-pressure washdowns, sanitation chemicals, and long continuous operating hours. The facility needed durable wiring that could withstand moisture, support heavy-duty machinery, and minimize costly downtime.
Solution: BTC provided high-quality control cables, power cables, and moisture-resistant accessories designed specifically for food processing and packaging lines. These solutions protected all wiring during daily cleaning cycles and supported continuous machine operation.
Improved system reliability, fewer electrical faults, and significantly easier maintenance. The client valued BTC’s application-focused product recommendations and timely dispatch support.

Beverage Bottling Facility
Challenge: Needed flexible wiring solutions to support fast-moving machines and compact plant layouts. Poorly organized legacy cabling was making maintenance difficult and reducing operational line efficiency.
Solution: BTC supplied flexible wiring along with structured cable management solutions to support smooth machine movement and cleaner installations. The improved layout made inspections quicker and reduced cable mechanical stress during continuous operation.
Improved production line throughput, a cleaner plant environment, and reduced overall maintenance time. The customer appreciated BTC’s practical solutions and industry expertise.
Cold Storage Facility
Challenge: Facing electrical performance degradation and condensation issues due to low sub-zero temperatures and high moisture levels, which risked temperature fluctuations in stored perishables.
Solution: BTC analyzed the operational environment and supplied power and control cables along with sealed accessories specifically engineered to perform reliably in cold and damp conditions, ensuring a stable power supply to refrigeration compressors.
Achieved uninterrupted refrigeration operations and enhanced system longevity. The client expressed strong confidence in BTC’s customized product specifications.
Frequently Asked Questions (People Also Ask)
Technical guidance on food-grade cables, washdown resistance, hygiene regulations, and installation durability.
Contact Bharat Trading Corporation
Need help choosing the right product or have a specific requirement? Our team is here to assist you.